Category Archives: Uncategorised

A Brief History of Lasers in Industry: From Scientific Breakthrough to Precision Engineering

Lasers have transformed modern industry, enabling manufacturers and engineers to achieve levels of precision, speed and control that were once difficult to imagine. Today, laser technology plays an important role in everything from manufacturing and aerospace engineering to quality control, non-destructive testing and industrial safety.

However, the industrial applications we rely on today began with a relatively simple scientific breakthrough. Over the past six decades, advances in laser design, power and optical control have turned the laser from an experimental laboratory device into an indispensable tool across numerous industries.

In this article, we explore the history of lasers in industry, the key developments that shaped their adoption and how laser technology continues to influence modern engineering.

1960: The Birth of the Laser

The story of laser technology began on 16 May 1960, when American physicist Theodore Maiman successfully demonstrated the first working laser using a synthetic ruby crystal.

The invention followed decades of scientific research into the principles of stimulated emission, a process first described theoretically by Albert Einstein in 1917. The development of a working laser made it possible to generate a highly concentrated, directional beam of light with properties that could be exploited for practical applications.

Initially, lasers were primarily used in scientific research. Their potential for industrial applications, however, quickly became apparent. A precisely controlled beam of light offered a new way to deliver energy to a specific point without the physical contact required by conventional tools.

This opened the door to new possibilities in materials processing, measurement and inspection.

The 1960s: Early Industrial Applications

During the 1960s, researchers began investigating how lasers could be used to cut, drill and modify materials.

The development of the carbon dioxide (CO₂) laser in 1964 was particularly significant. Its ability to generate relatively high continuous power made it a promising technology for industrial materials processing.

One of the most important early milestones occurred in May 1967 at The Welding Institute (TWI) in Cambridge, UK. Peter Houldcroft demonstrated how a focused CO₂ laser beam, combined with oxygen assist gas, could cut through a 1 mm thick sheet of steel.

This experiment helped establish the foundations of modern laser cutting.

Early systems were relatively large, expensive and technically demanding to operate. Nevertheless, they demonstrated that lasers could offer an alternative to conventional cutting and machining methods, particularly where accuracy and repeatability were important.

The 1970s: Lasers Enter the Factory

By the 1970s, industrial laser technology was progressing from experimental applications towards practical production equipment.

Manufacturers began exploring laser cutting and welding for applications where traditional processes could struggle to deliver the required precision or consistency. The automotive and aerospace industries were particularly interested in the technology, as both sectors required accurate processing of components and materials.

Early industrial laser systems were often complex and costly, with reliability and operating requirements limiting their widespread adoption. However, improvements in laser power, beam delivery and machine design gradually made the technology more practical for production environments.

During this period, laser processing began to establish its place within modern manufacturing, paving the way for the more sophisticated systems that would follow.

The 1980s: Wider Adoption and New Applications

The 1980s marked an important period of growth for industrial laser applications.

As laser systems became more capable and reliable, their use expanded beyond metal cutting and welding. Laser drilling, marking and engraving became increasingly practical, while developments in materials processing opened up applications involving plastics, textiles, rubber and other materials.

Computer-controlled machinery also helped manufacturers take advantage of the laser’s precision and repeatability. By combining focused laser beams with increasingly sophisticated motion-control systems, manufacturers could produce intricate shapes and detailed features with greater consistency.

Lasers were no longer simply an emerging technology. They were becoming established tools in industrial production, supporting greater automation and more demanding engineering requirements.

The 1990s and 2000s: Precision, Automation and Optical Innovation

During the 1990s and early 2000s, advances in computing, optical components and control systems further expanded the capabilities of industrial lasers.

Computer-aided design and computer numerical control (CNC) enabled digital designs to be translated into precise manufacturing operations. This helped make laser processing suitable for increasingly complex components and repeatable production runs.

At the same time, laser technology continued to develop for applications beyond cutting and welding.

Lasers became increasingly important in:

  • Industrial measurement: Supporting precise dimensional measurements and alignment.
  • Quality control: Helping manufacturers identify defects and verify component accuracy.
  • Surface processing: Enabling controlled treatment, cleaning and modification of materials.
  • Marking and traceability: Applying durable identification codes and markings to components.
  • Scientific and engineering research: Providing controlled light sources for testing, analysis and measurement.

These developments highlighted an important advantage of laser technology: it is not limited to changing materials. It can also provide a highly controlled means of examining, measuring and understanding them.

The 2010s: The Rise of Fibre Lasers

One of the most significant developments in modern industrial laser technology has been the growing adoption of fibre lasers.

Although the underlying concepts of fibre laser technology date back several decades, advances in optical fibres, laser diodes and manufacturing techniques helped make high-power fibre laser systems increasingly practical for industrial use.

Fibre lasers offer several advantages, including excellent beam quality, efficient operation and relatively compact designs. These characteristics have made them particularly attractive for applications such as metal cutting, welding, marking and precision processing.

Their adoption has helped manufacturers improve processing speeds and energy efficiency in suitable applications, while expanding the range of tasks that can be performed using laser technology.

Other laser types, including CO₂ and solid-state lasers, remain important where their particular wavelengths and operating characteristics suit the material or application.

The key development has therefore not been the replacement of every older laser type, but the expansion of the available technologies to meet different industrial requirements.

Today: Lasers Beyond Manufacturing

Modern laser technology is used across a much broader range of industrial and engineering applications than early researchers could have anticipated.

While cutting, welding and marking remain important uses, lasers are also valuable in optical measurement, industrial inspection and non-destructive testing (NDT).

For example, laser-based measurement techniques can help engineers assess component dimensions, alignment and surface characteristics. Advanced optical inspection methods can also reveal information about a component’s condition without necessarily requiring it to be dismantled or damaged.

One example is laser shearography, an optical technique used to detect surface deformation and identify potential defects in materials and structures. It can be useful in applications where maintaining the integrity of the item being inspected is essential.

As industrial systems become more sophisticated, the importance of reliable optical equipment, accurate measurements and appropriate laser safety measures continues to grow.

Lasers are also increasingly integrated into automated production environments, where their performance depends on the quality of the optical system, the control equipment and the procedures used to operate them.

The Importance of Laser Safety

As laser technology has become more powerful and widely used, laser safety has become an essential consideration for industrial organisations.

Laser hazards vary according to the laser’s wavelength, power, operating mode and application. Direct exposure to certain laser beams can cause serious eye injuries or skin damage, while reflections may present additional risks in some environments.

Appropriate protective measures depend on a thorough assessment of the specific equipment and working conditions. These measures may include suitable protective eyewear, controlled access, beam enclosures, warning systems and appropriate staff training.

Optical components and protective equipment must also be selected for the intended wavelength and operating conditions. Not all protective products are suitable for every laser application.

Understanding these requirements helps organisations use laser technology effectively while protecting employees, equipment and working environments.

The Future of Industrial Laser Technology

The development of industrial lasers is continuing, with ongoing advances in beam control, automation, optical sensing and data processing.

Manufacturers are exploring increasingly precise laser processes, while engineers are developing new ways to use optical techniques for inspection, monitoring and quality assurance.

As production systems become more automated and component tolerances become increasingly demanding, the ability to measure, process and inspect materials accurately will remain important.

Laser technology is well positioned to support these requirements, provided that systems are designed, integrated and operated appropriately for their intended applications.

Conclusion

From the first working laser in 1960 to today’s advanced fibre lasers and optical inspection systems, the history of industrial lasers is one of continual innovation.

What began as a scientific breakthrough has become a technology that supports precision manufacturing, engineering measurement, industrial inspection and workplace safety across numerous sectors.

Understanding this history helps explain why lasers are now such an important part of modern industry — and why continued developments in optical engineering will remain central to their future.

At Laser Optical Engineering Ltd, we recognise the importance of precision optics and reliable laser technology in demanding industrial environments. Whether supporting optical inspection, measurement or laser safety requirements, selecting the right equipment for the application is essential to achieving dependable results.

To learn more about our optical engineering capabilities, laser safety products and industrial solutions, explore the Laser Optical Engineering website.

Laser Shearography for Non-Destructive Testing (NDT): How It Works and Why It Matters

Non-destructive testing (NDT) plays a critical role in modern engineering, allowing industries to evaluate the integrity of materials and components without causing damage. One of the most advanced optical NDT methods available today is laser shearography, a powerful technique that delivers fast, full-field inspection of complex structures.

At Laser Optical Engineering, shearography is used to detect hidden defects in composites, bonded structures, and advanced materials with exceptional accuracy and efficiency.

What Is Laser Shearography?

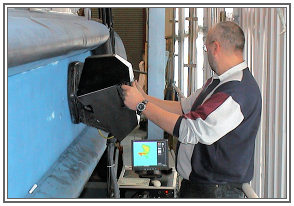
Laser shearography is an interferometric inspection method that uses coherent laser light to measure how a surface deforms under stress. Instead of looking directly for cracks or voids, it identifies microscopic deformation differences that occur when a material is loaded.

A typical inspection involves:

  • Illuminating the component with a laser
  • Capturing a reference image of the surface
  • Applying a small controlled stress (such as heat, vacuum, or mechanical load)
  • Capturing a second image under load
  • Comparing both images to reveal abnormal strain patterns

Defects such as delaminations, disbonds, impact damage, and voids cause localized changes in stiffness, which appear clearly in the shearography image as fringe pattern disturbances.

How Laser Shearography Works in Practice

Shearography systems measure the gradient of surface displacement rather than just surface movement. When a material is intact, it deforms uniformly under stress. However, if there is a subsurface flaw, that region responds differently.

This difference in behaviour is captured in real time, producing a visual map of strain anomalies. Because the system captures a full area at once, it is highly efficient for inspecting large or complex surfaces such as:

  • Aircraft composite panels
  • Wind turbine blades
  • Automotive bonded structures
  • Rubber components and tyres
  • Marine and aerospace sandwich panels

Benefits of Laser Shearography in NDT

Laser shearography offers a range of advantages over traditional inspection methods such as ultrasonic testing or dye penetrant inspection.

1. Full-field inspection

Unlike point-by-point methods, shearography inspects large areas in a single capture, significantly reducing inspection time.

2. Non-contact and non-invasive

No physical contact or coupling media is required, meaning delicate or sensitive surfaces remain completely undisturbed.

3. Extremely fast results

Defects are revealed in real time, allowing immediate decision-making during inspection.

4. High sensitivity to subsurface defects

Shearography is particularly effective at identifying hidden flaws such as:

  • Delaminations
  • Disbonds in adhesive joints
  • Core damage in sandwich structures
  • Impact damage not visible on the surface

5. Suitable for industrial environments

Modern systems are robust and tolerant of vibration, making them suitable for both laboratory and field use.

6. Improved quality assurance

By revealing defects early in production or maintenance, shearography helps reduce failures, rework, and costly downtime.

Why Industries Use Laser Shearography

Industries that rely on high-performance composite materials benefit significantly from shearography because it provides:

  • Rapid inspection of large structures
  • Reduced maintenance costs
  • Improved safety and reliability
  • Non-destructive evaluation of critical components
  • Better lifecycle monitoring of assets

It is widely used in aerospace, wind energy, automotive manufacturing, and advanced materials engineering.

The Value of Laser Optical Engineering Solutions

Laser Optical Engineering develops advanced shearography systems designed for precision, reliability, and ease of use. These systems help engineers and inspectors identify hidden structural issues quickly and accurately, supporting safer and more efficient manufacturing and maintenance processes.

Conclusion

Laser shearography is one of the most effective modern NDT techniques for inspecting composite and bonded structures. By visualising strain anomalies rather than direct damage, it provides a powerful way to detect hidden defects before they become critical failures.

As industries continue to adopt advanced materials, shearography will remain an essential tool for ensuring structural integrity, safety, and performance.

Finding Our Way Directory

Web Site Directory

Laser Visor Strips — Advanced Eye Protection from Laser Optical Engineering Ltd

In environments where lasers are used, from public safety operations to aviation, protecting the eyes from intentional or accidental laser exposure is critical. Laser Optical Engineering Ltd offers a proven solution with its Laser Visor Strips and Anti-Dazzle Glasses, expertly designed to safeguard the vision of officers, pilots and other professionals without restricting their performance or field of view.

Effective Protection Against Laser Pointer Threats

Working in collaboration with the Police Service of Northern Ireland (PSNI) and the UK Home Office’s CAST unit, Laser Optical Engineering has developed visor strip technology that significantly reduces the risk posed by laser pointer attacks. These strips are especially useful in scenarios where public order officers might be targeted by laser beams during operations.

The strips mount easily above the wearer’s normal line of sight on existing helmet visors. When a laser beam is directed towards the officer, a simple lowering of the head allows the visor strip’s filter to block the harmful light, providing eye protection while still allowing full mobility and situational awareness.

Each visor strip comes with clear fitting instructions, a lens cleaning wipe, and can be positioned for optimum protection based on the individual user’s needs. Laser Optical Engineering also offers a professional fitting service for added convenience.

Innovative Anti-Dazzle Glasses for Pilots

In addition to visor strips, Laser Optical Engineering supplies Anti-Dazzle Glasses designed to protect pilots’ eyes from direct laser exposure during flight phases such as take-off and landing. These glasses incorporate a specialised filter that sits between the pilot’s eye and the laser light source. The protective filter is engaged naturally by tilting the head, an instinctive reaction, which minimises disruption to the pilot’s vision.

One of the key benefits of these glasses is that they can be worn comfortably over standard prescription eyewear, ensuring important eye protection without compromising visibility or comfort.

Why Choose Laser Visor Strips?

  • Trusted Performance – Developed alongside PSNI and UK Home Office teams.
  • Simple Installation – Designed to adapt easily to existing helmet systems.
  • User-Centred Design – Full instructions and optional fitting service included.
  • Enhanced Safety – Offers eye protection during laser pointer attacks without hindering operational duties.

Whether for law enforcement, aviation or other settings where laser exposure is a concern, Laser Optical Engineering Ltd’s laser vision protection products are a reliable choice that balance safety, usability, and performance.

B2B Listings

Understanding Laser Shearography in Industrial Inspection

What Is Laser Shearography?

Laser shearography is an advanced non-destructive testing (NDT) technique that uses laser interferometry to detect hidden flaws within materials and components. Instead of relying on physical contact or simple visual inspection, it provides a full-field, high-resolution image of surface and subsurface defects. The process involves projecting laser light onto a surface, then applying a small amount of stress through heat, vacuum, or mechanical load. Any underlying defects cause microscopic deformations, which the shearography system captures as fringe patterns. These patterns clearly reveal the location and severity of faults such as delaminations, cracks, and disbonds.

How It Works

When a material is illuminated by coherent laser light, the reflected beams create an interference pattern that represents the surface’s optical characteristics. By comparing two states, before and after stress is applied, laser shearography detects even the smallest changes in the surface structure. The result is a real-time visualisation of strain anomalies that indicate internal damage. Because the system captures data from an entire area at once, large surfaces can be inspected quickly and accurately.

Industrial Applications

Laser shearography has proven invaluable across a range of industrial and manufacturing sectors. It is widely used for:

  • Aerospace and Defence: Inspecting composite aircraft panels, bonded joints, and honeycomb structures for delamination or debonding.
  • Automotive and Motorsport: Testing lightweight carbon fibre components, tyres, and bonding integrity in structural parts.
  • Wind Energy: Evaluating turbine blades and composite sections for subsurface defects that could affect performance.
  • Rubber and Composites Manufacturing: Ensuring quality control during production without interrupting workflow.

Its ability to perform on-site, non-contact inspection makes it ideal for both laboratory testing and in-field maintenance.

Benefits of Using Laser Shearography

Compared with conventional NDT techniques such as ultrasonic or dye penetrant testing, laser shearography offers several key advantages:

  • Full-field inspection: Captures large surface areas in a single measurement.
  • High sensitivity: Detects minute subsurface defects invisible to the naked eye.
  • Fast and efficient: Produces results in real time with minimal setup.
  • Non-contact and non-destructive: No risk of damage to delicate materials.
  • Vibration-tolerant: Can be used effectively in industrial or outdoor environments.
  • Digital traceability: Results can be archived and compared for long-term monitoring.

Advancing Quality and Reliability

For industries where structural integrity and reliability are critical, laser shearography delivers a powerful, efficient, and precise inspection solution. By enabling early defect detection and reducing the need for rework, it helps manufacturers improve quality, extend component life, and maintain safety standards.

Laser Optical Engineering Ltd continues to lead the way in the development and application of shearography systems, supporting industries that demand the highest levels of precision and assurance in non-destructive testing.

UK Manufacturers – List of Industrial Manufacturers

Finding Our Way Directory
Expotural.com

Enhancing Laser Safety in Commercial Applications

The prominence of laser technology has grown across diverse sectors, including medicine, industry, research, and entertainment. However, the potential harm of laser radiation to human well-being has become evident. The mishandling of lasers can lead to injuries and property harm. Consequently, adhering to laser safety protocols and standards is imperative to safeguard both people and the environment. The British Standard BS EN 60825 stands as a pivotal guideline for laser safety. Thus, ensuring laser safety, employing interlock systems, using safety cabinets, and complying with BS EN 60825 have become paramount.

The Significance of Laser Safety

Laser radiation can inflict damage on human skin and eyes, resulting in temporary or permanent impairment. The extent of injury depends on factors like wavelength, power, and exposure duration. For example, high-power laser exposure can cause blindness, while lower-power instances can lead to skin burns. Beyond this, laser radiation can even ignite flammable materials, causing fires and explosions. Besides injury and property risk, laser radiation can disrupt electronic devices. Sensors, cameras, and other electronic components can be compromised by laser interference. Hence, guaranteeing safe laser usage is essential to avert accidents, injuries, and equipment damage.

Understanding British Standard BS EN 60825

BS EN 60825, a British Standard, offers comprehensive laser safety guidance. It encompasses various laser products, ranging from pointers to medical, industrial, and research laser equipment. This standard covers aspects such as hazard classification, labelling, and user training. The most recent version, BS EN 60825-1:2014, was published in 2014.

Hazard Classification within BS EN 60825

BS EN 60825 categorizes lasers into four hazard classes based on potential risks to human eyes and skin:

Class 1: Safe lasers emitting non-hazardous radiation below the maximum permissible exposure (MPE) limit.

Class 2: Low-risk lasers emitting visible radiation that poses no harm if exposure remains under 0.25 seconds, though prolonged exposure can damage eyes.

Class 3R: Moderate-risk lasers emitting visible radiation that can harm eyes if exposure is extended. They are also hazardous when optical instruments direct the beam into eyes.

Class 4: High-risk lasers emitting radiation capable of damaging eyes and skin, while also presenting a fire hazard. They demand specific precautions for safe usage.

Labelling

The standard mandates laser products to carry specific information on labels, including hazard class, maximum output power, and wavelength. Labels must also feature warning symbols and instructions for safe handling and use. These labels must be visible, easily readable, and affixed to the laser product or packaging.

Laser Safety Training

The standard necessitates proper training in laser safety and handling for users. This education should cover hazards of laser radiation, secure operating procedures, and emergency responses. Training should address the specific hazards tied to the utilized laser product. Documentation and periodic reviews of the training are recommended.

Interlock Systems

Interlock systems are pivotal in ensuring laser safety. They prevent laser operation when specific safety conditions are unmet. These systems can be mechanical or electrical and integrated into laser products or control systems.

Mechanical interlocks employ physical barriers (doors, covers) to bar access to the laser beam. For instance, a laser safety cabinet might halt laser operation if its door is open. This confines the laser within the cabinet, averting risks.

Electrical interlocks rely on sensors and switches to detect hazards, halting laser operation when such risks are present. For instance, an electrical interlock may identify misalignment or faulty cooling. If these conditions persist, the interlock prevents laser use.

Interlock systems are pivotal for high-power laser systems, fortifying safety against accidents and injuries. They can be tailored for specific applications and safety prerequisites, often necessitating multiple systems.

Laser Safety Cabinets

Laser safety cabinets offer secure environments for laser systems. These enclosures prevent laser radiation from escaping, proving crucial for high-power or high-risk laser systems.

Crafted from laser-resistant materials like metal or plastic, cabinets often contain laser-absorbing linings to minimize radiation reflection. Interlock-equipped doors thwart laser operation if open.

Laser safety cabinets provide controlled environments, often featuring ventilation for heat removal and prevention of hazardous gas buildup. Fire suppression systems further enhance protection.

These cabinets are pivotal for high-risk laser systems, providing controlled surroundings for laser operation while containing radiation. This approach ensures both effective laser use and safety.

The Mats Directory
Lider Press Directory
SeekWebsites DIRECTORY Visit BlogAdda.com to discover Indian blogs
businesses
MCBN.org
Abiz Directory
In-SLA Directory

ISO 17025 manual

LiveCycle Portal

LinkTo.Directory